Introduction: A Clear Choice or a Hidden Compromise?
Here’s the truth: visual decisions at retail are made in seconds. Square perfume bottles sit up straight, catch light on the edges, and signal order and luxury. Picture a product launch, shelf-ready by Friday, with a buyer who scrolls SKUs faster than you can say “MOQ.” Internal reports show that shape alone can drive first-touch interest by a third—yet breakage and misfit can erase that gain overnight. So the big question is simple: are square forms your best move, or do they hide more operational risk than they reveal (especially when timelines pinch)? We’ll anchor on form, function, and the math of tolerances—funny how that works, right? The goal is to distinguish aesthetic appeal from process reality without jargon overload, but still be precise and fair. Short answer: it depends on how you spec, test, and pack. Long answer: let’s unpack the friction points and the upside, side by side, with real production cues and decision-ready criteria—then you can judge the fit for your line. Let’s move into the specifics and see where the edges cut, and where they shine.
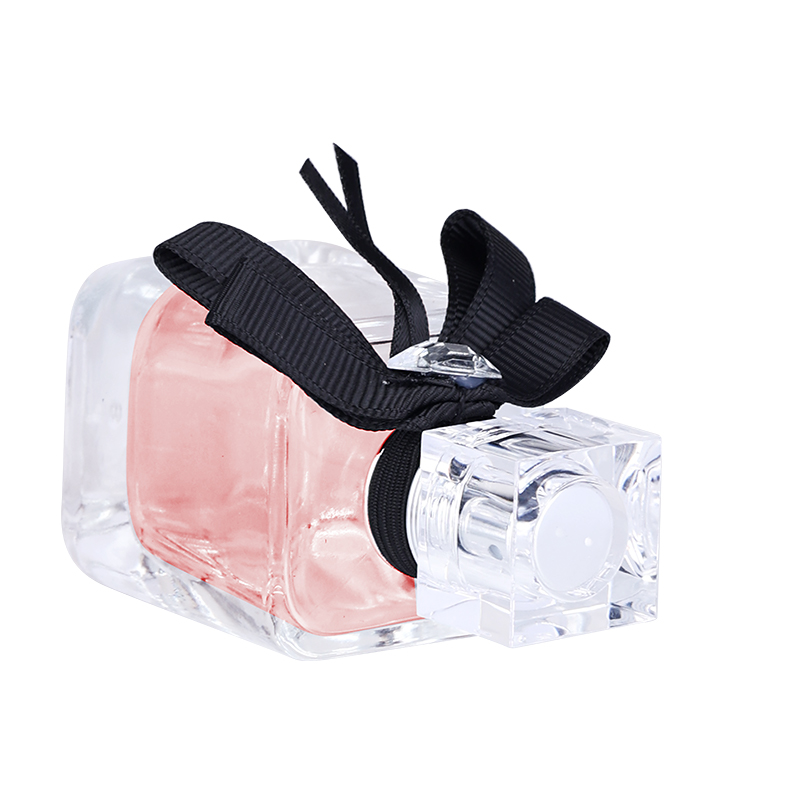
Part 2: The Hidden Friction Behind Clean Lines
Why do tolerances matter?
At the component level, a china square perfume glass bottle is a geometric promise that your pump, cap, and label must keep. Corners concentrate stress and magnify gaps; that’s basic geometry, not opinion. In practice, tolerance stack-up across the GPI neck finish, the crimp pump ferrule, and the cap cavity can skew alignment by a millimeter. On a round bottle, it hides. On a square, it shouts. Edge crispness also depends on the annealing lehr curve; rush that profile and you risk microstrain that turns into chipping during pump crimping or transit. Hot end coating helps glide the glass through the line; without a proper cold end coating, scuffing ruins that expensive spray lacquering or silkscreening. Look, it’s simpler than you think: the squarer the silhouette, the tighter your upstream controls have to be.
There’s more. Fill height variation feels bigger in a square because the flat face is a ruler—your consumer’s eyes become QC. Any warp on a label—caused by corner radius drift—breaks the visual grid. And caps with a rectangular shroud? If thread pitch drifts, you get that dreaded “off-axis” face. Freight math is also tricky: cartons cubed for squares look efficient, but corner-protective inserts add volume, and you may end up with no net gain—funny how that works, right? If your AQL plan is light on dimensional checks, you’re gambling with a design that does not forgive. The fix is not exotic: better neck gauges, corner radius specs, and a verified crimp window reduce rejects fast, often more than any last-minute carton tweak.
Part 3: Comparative Outlook and What’s Next
What’s Next
Looking forward, two shifts help square formats play nicer with ops. First, process control is getting smarter. Vision systems now read wall thickness at corners and track finish concentricity in-line (no slow sampling). Pair that with tuned annealing profiles and you stabilize edges without over-tempering. Second, surface engineering is more consistent. Newer cold end coating recipes cut scuff rates after spray lacquering by double digits, which keeps flat faces clean under retail lights. If you’re sourcing china square glass perfume bottles, ask how mold venting and cavity balancing are managed; those two details often decide whether caps sit flush or look crooked. Compare this to round formats and you’ll still see a wider process window with rounds, but squares close the gap when specs are disciplined and QC is real-time. The net result is less drama at crimp, cleaner label lines, and a shelf face that reads premium without fragile edges. And yes, the cube math on freight only works when inserts are die-cut to the actual corner radius—it’s not just about outer dims.
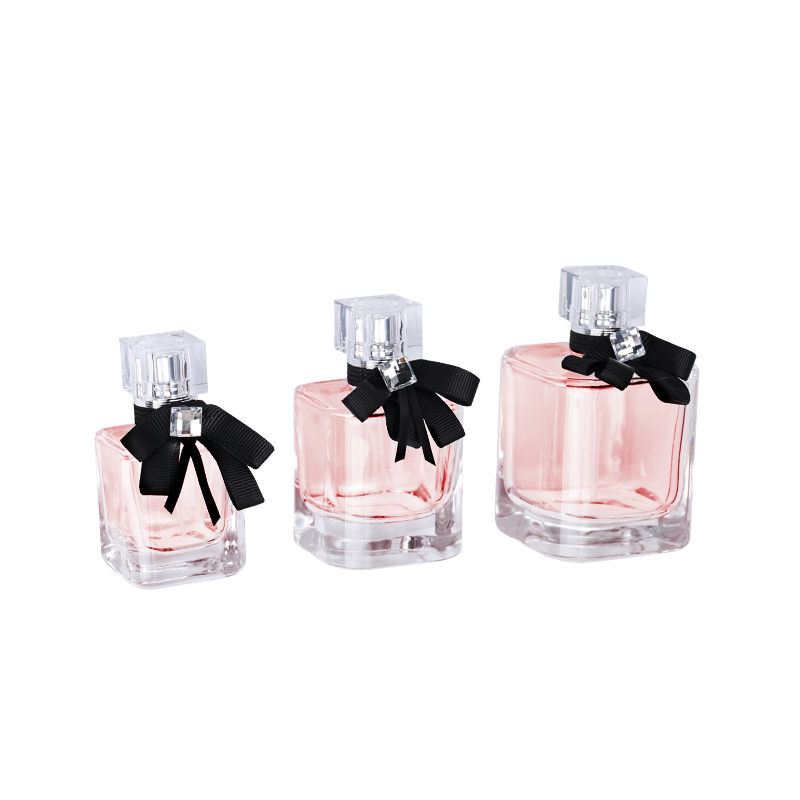
So how should you choose? Use three metrics. 1) Alignment fidelity: cap-to-panel parallelism after crimp, measured across a full AQL pull. 2) Edge integrity: chip and scuff rate post-line and post-ship, tracked by coating type and annealing curve. 3) Visual precision: fill height and label skew tolerance, verified on flat faces under 500–1000 lux. If a supplier shows repeatable control on those, the square silhouette is more than a look—it’s a reliable platform. If not, go round or refine the spec before artwork. Either way, the comparison is clearer when you measure the right things, not just the glass weight. For deeper engineering notes and supplier dialogue, see NAVI Packaging.